Dishwasher manufacturing depends on more than motors, pumps, and attractive control panels. Pressed stainless-steel tubs, door skins, brackets, and reinforcement parts must fit consistently through assembly. That is where a reliable Dishwasher Stamping Die supplier can affect production speed, scrap levels, and the finish customers see. The details matter.
Grand View Research’s Global Dishwasher Market Size, Share & Trends Analysis Report estimated the market at about US$30.6 billion in 2023 and forecast 7.8% compound annual growth through 2030. This is a market estimate, not a guarantee of future orders. Still, it signals why manufacturers are watching capacity and tooling resilience. ENERGY STAR’s Version 7.0 specification also sets a 3.2-gallon-per-cycle water-use limit for standard residential dishwashers. Efficiency targets do not dictate die design, but they add pressure to deliver dependable products without waste.
This 2026 overview compares suppliers through practical criteria: press and toolmaking capability, material expertise, engineering support, quality controls, lead times, and after-sales service. A polished website proves little. Ask for sample-part measurements, tool tryout records, and clear maintenance plans. Where available, verify certifications and customer references directly. Supplier rankings can also hide important differences: one company may excel at complex transfer dies, while another suits high-volume progressive stamping. No shortlist fits every factory. Use the comparisons as a starting point, then test each supplier against your part geometry, production volume, and regional support needs.
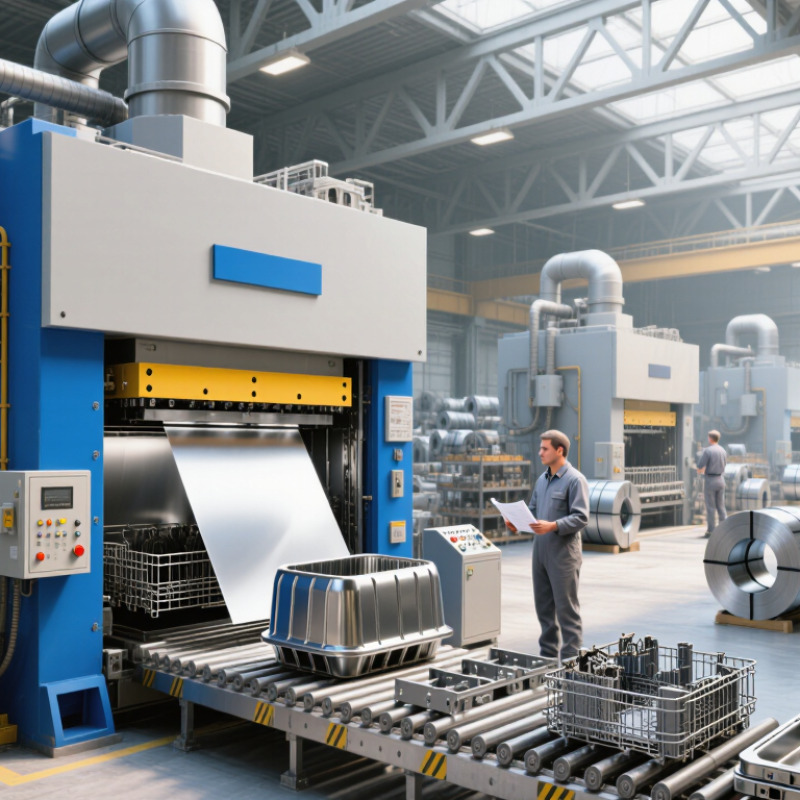
Dishwasher stamping dies shape flat metal into parts used throughout an appliance. In a press, the die can cut, pierce, bend, or form stainless steel and coated sheet. These operations produce items such as tub panels, door supports, brackets, and mounting plates. Small details matter. A misaligned hole can complicate assembly later.
A well-designed die helps parts come off the press with consistent dimensions and clean edges. That consistency supports reliable fit around seals, fasteners, and adjoining panels. Die design also accounts for material thickness, springback, press capacity, and the intended production volume. Those details are easy to overlook when evaluating a tool from drawings alone.
Suppliers typically contribute to design review, tool construction, tryout, and maintenance planning. During tryout, sample parts reveal issues such as wrinkles, burrs, or uneven bends. Adjustments may be needed, even when the initial design looks sound. Fit is not automatic. A practical supplier should explain inspection methods, expected tool life, and how wear-sensitive areas will be serviced. Clear records of revisions and sample measurements make later troubleshooting easier. A die can meet its drawing and still create production headaches; real press conditions deserve careful review.
A supplier should be judged by repeatable part quality, not a polished presentation. Review dimensional inspection reports for formed panels, brackets, and door components. Ask how measurements hold across a full production run, not just a handful of samples. Die simulation is useful, but trial data matters more. Look for documented control of springback, burrs, and coil-thickness variation.
Market demand adds context. Fortune Business Insights estimated the global dishwasher market at USD 33.43 billion in 2023, with continued growth projected through 2032. That outlook makes production capacity and maintenance planning relevant. ENERGY STAR reports that certified dishwashers use about 12% less energy and 30% less water than standard models. Those targets can put pressure on formed-part fit and sealing surfaces, so suppliers should explain how die changes are validated.
Compare die life, changeover time, spare-part availability, and response time after a production issue. Request sample parts made on the intended press, using the specified material and thickness. Check that the supplier records revisions and links them to inspection results. A scorecard still misses things. Communication during a difficult tool trial can reveal more than a neat quotation. And the cheapest bid can become expensive if routine wear causes inconsistent parts.
Leading dishwasher stamping die suppliers in 2026 stand out through process control, not polished sales claims. They can explain how a die handles stainless-steel panels, tight radii, and repeated forming without excessive springback. Ask for sample parts, dimensional inspection records, and details about press compatibility. A useful supplier also discusses maintenance access and replacement inserts before production begins. Fit matters. Even a clean sample may not reveal tool wear after thousands of cycles, so ask how performance is monitored over time.
Tips: Share material grade, sheet thickness, target output, and critical dimensions before requesting a quote. Ask to review a stamped sample and its inspection results. Confirm who handles die trials, adjustments, and spare components. Clear answers are a good sign.
Compare suppliers on engineering support, lead-time transparency, and their ability to troubleshoot real production issues. A capable team should identify likely risks, such as wrinkles near a draw or uneven trimming, and explain how it would test solutions. Check whether proposed tolerances match the part’s function; tighter is not automatically better. Some details may still need revision after the first trial. That is normal, but changes should be documented and verified with measured parts. A supplier that welcomes technical questions is often a safer choice than one promising perfect results without evidence.
Dishwasher stamping dies must hold dimensions across repeated cycles, heat, vibration, and changing sheet-metal conditions. A capable supplier explains how die design supports the part’s geometry, material thickness, and expected production rate. Ask to review forming simulations, tolerance plans, and maintenance access before approving a design. Small details matter, such as whether operators can replace a worn insert without removing the full die.
Tooling quality is visible in more than a polished surface. Check machining records, inspection methods, and trial-run results for evidence of repeatability. A practical review might compare sample panels from several press strokes, measuring hole positions and flange angles. The supplier should also describe how it handles springback or wrinkling when trial parts fall outside specification. Good answers are specific. Vague assurances are not.
Production support can separate a reliable partner from a shop that only delivers hardware. Discuss spare inserts, repair turnaround, setup guidance, and response times during ramp-up. Ask who will attend the first production trial and how process changes are documented. These commitments should be clear, not assumed. Still, no scorecard predicts every factory condition; a supplier’s strengths may look different once the die meets the actual press, coil, and operator routine. That uncertainty deserves a real trial, not just another spreadsheet.
For a dishwasher program, supplier selection should start with the part, not the sales pitch. Share drawings, material grades, sheet thicknesses, expected volumes, and the press specifications the die must fit. A supplier should explain how its team will review forming risks, check tolerances, and plan tool tryout. Clear answers matter.
Ask how the die will handle features such as deep-drawn tubs, stiffening ribs, and pierced mounting points. Request evidence of inspection methods, sample-part checks, and corrective-action tracking. Confirm who owns design changes and how revisions reach the toolroom. Small details add up.
Compare realistic lead times, spare inserts, maintenance guidance, and support during production ramp-up. A low initial quote can leave important costs unclear, especially if tryout rounds or later modifications are excluded. Ask for a written scope. Then compare like with like.
If possible, review parts from a comparable application and speak with the engineers who will support your program. Check whether the supplier can coordinate with your press team on feed direction, shut height, and safe handling. Early estimates are rarely perfect; production trials may reveal an overlooked wrinkle or springback issue. That is useful information, if the supplier documents it and responds with a practical adjustment. A polished presentation helps, but consistent communication and measurable process controls are stronger signs of fit.
Use this supplier-selection scorecard to compare qualified candidates without relying on unverified rankings. The weights are suggested evaluation priorities, not published market data; adjust them to fit your part, volume, and risk requirements.
| Evaluation Area | Suggested Weight | Evidence to Request | Dishwasher-Program Relevance | What a Strong Candidate Demonstrates |
|---|---|---|---|---|
| Part and process engineering | 15% | Design-for-manufacturing review, forming simulation where appropriate, risk analysis, and documented design-change control. | Helps identify forming, springback, material, and fit risks before tool release. | Reviews the part drawing and material specification, documents assumptions, and proposes measurable validation checks. |
| Die design and build capability | 15% | Die concept and layout, tool component specifications, build schedule, and examples of comparable tooling scope. | Tool design must match the part geometry, production method, press, and planned output. | Explains the proposed die type, critical features, maintenance access, and the basis for the quoted build timeline. |
| Press and line compatibility | 12% | Press tonnage, bed and bolster dimensions, shut height, stroke, feed method, and available line specifications. | Confirms that the die can be installed and run on the intended production equipment. | Checks all key machine interfaces against the receiving plant's press data before finalizing the tool design. |
| Quality system and traceability | 12% | Current quality-system certificate and scope, inspection plans, calibration controls, nonconformance process, and material traceability records. | Supports consistent tool build quality and controlled verification of stamped parts. | Provides verifiable records and explains how inspection results and corrective actions are managed. ISO 9001 certification may be relevant; verify the certificate and scope directly. |
| Tryout and dimensional validation | 12% | Tryout plan, sample-part inspection results, measurement method, corrective-action log, and agreed acceptance criteria. | Confirms that the die produces parts that meet drawing requirements under defined conditions. | Uses customer-approved drawings and measurement methods, records trial revisions, and obtains approval before production release. |
| Production readiness and capacity | 10% | Capacity calculation based on the agreed cycle, shift pattern, planned maintenance, staffing, and material supply. | Tests whether the supplier can support the program's forecast and delivery schedule. | Shows assumptions behind output commitments and has a documented plan for ramp-up and bottleneck management. |
| Tool maintenance and spare parts | 8% | Preventive-maintenance plan, wear-part list, recommended spares, repair process, and tool ownership and storage terms. | Reduces avoidable downtime and clarifies how production tooling will be supported over its service life. | Defines maintenance intervals, response responsibilities, spare-part lead times, and access to tool documentation. |
| Program management and communication | 7% | Named project contacts, milestone schedule, meeting cadence, escalation path, and change-request workflow. | Keeps engineering, tooling, procurement, and plant teams aligned from kickoff through launch. | Reports progress against milestones and communicates risks, decisions, and schedule changes promptly. |
| Total cost and commercial clarity | 5% | Itemized quotation covering design, build, tryout, modifications, freight, installation support, and exclusions. | Makes bids comparable and helps identify costs that may otherwise appear after award. | States assumptions, payment milestones, ownership terms, warranty coverage, and the process for out-of-scope changes. |
| Delivery and logistics risk | 4% | Origin, shipping plan, packaging method, customs responsibilities where applicable, and delivery contingency plan. | Helps assess timing, transport protection, and handoff requirements for the die and trial parts. | Provides a realistic delivery plan and assigns responsibilities for transport, documentation, and receiving-site coordination. |
| Total suggested weight | 100% | Score each supplier from 1 (weak evidence or significant gaps) to 5 (strong, verified evidence); multiply each score by its weight to create a program-specific comparison. | ||
Note: This is a supplier-selection framework, not a verified ranking of individual companies. Confirm certificates, references, equipment capability, and commercial terms directly with each candidate. IATF 16949 is an automotive-sector quality management standard and should be requested only when relevant to the customer's requirements or contract.